Mechanical Engineering | 3D Scanning | 3D Modelling
Tag: mining-chpp
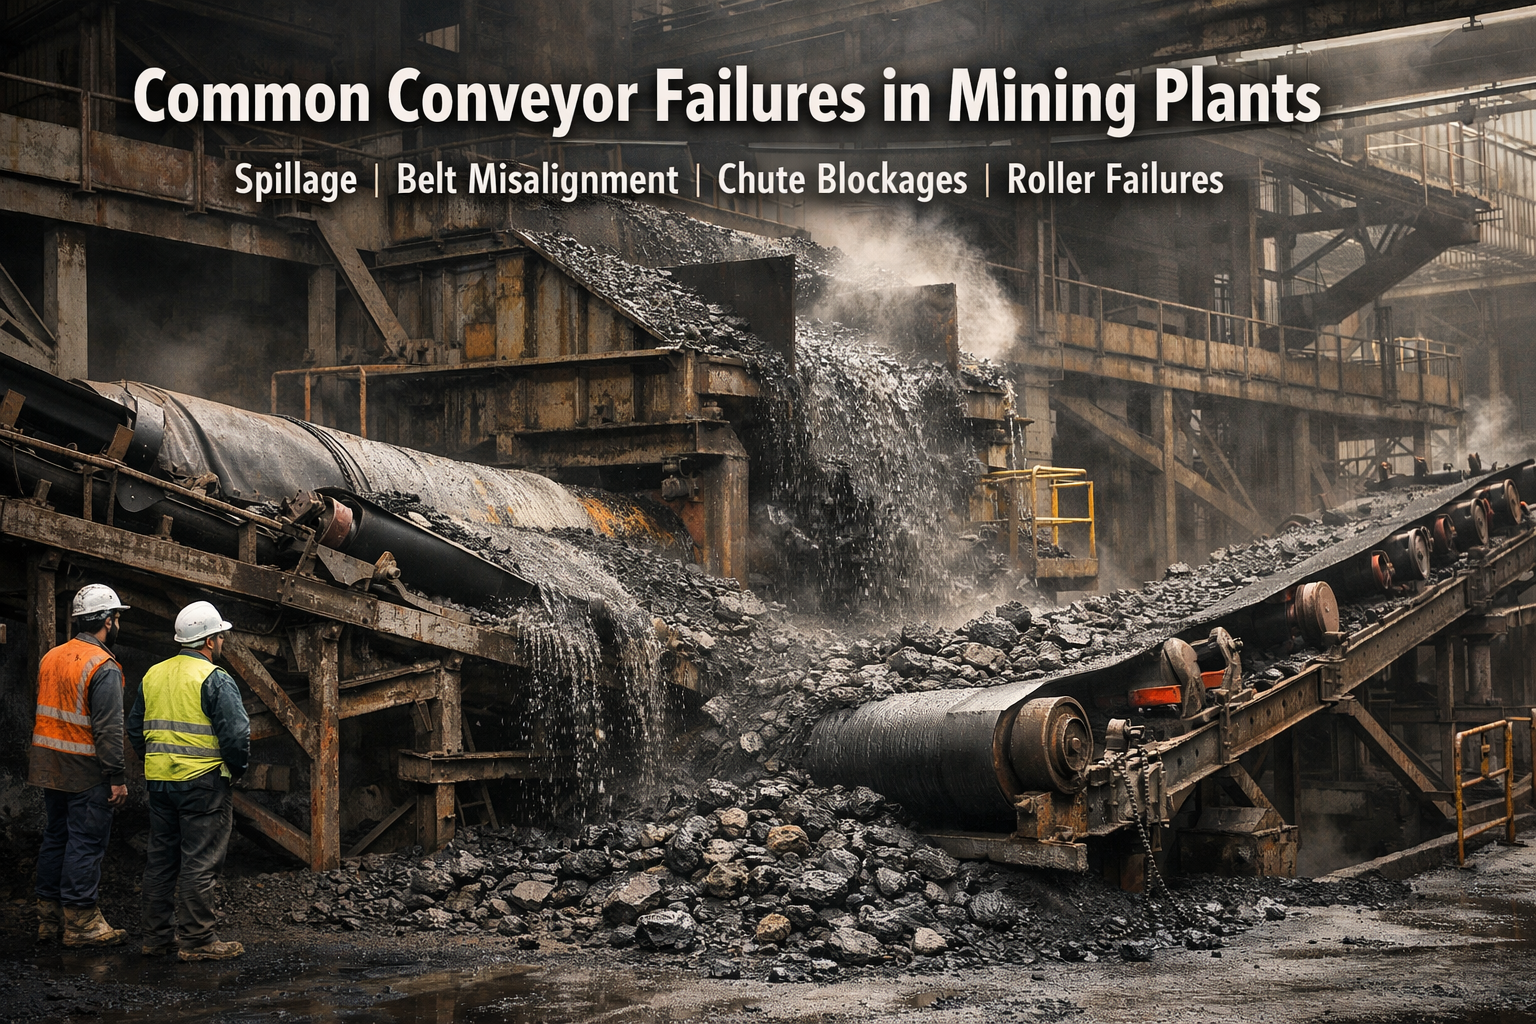
Hamilton By Design provides mechanical engineering, 3D LiDAR scanning and CAD support for coal handling and preparation plants throughout Australia.
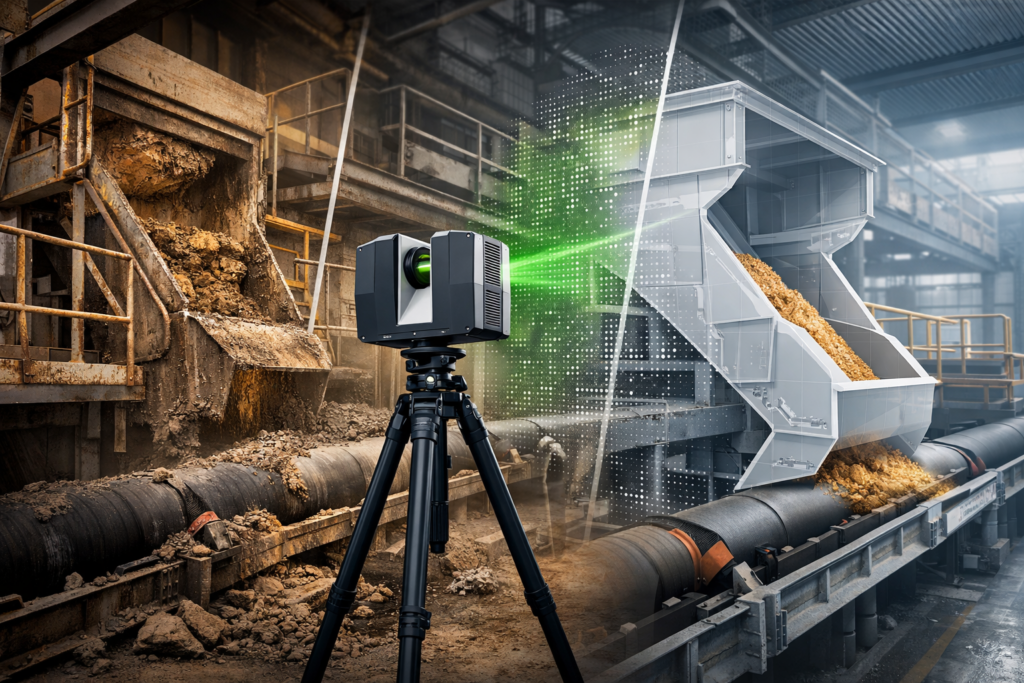
CHPP projects frequently involve modifications to existing conveyors, transfer chutes, bins, screens, tanks, pumps, pipework, platforms and other fixed plant assets. Accurate as-built information is particularly important when new equipment must connect to or fit around operating plant.
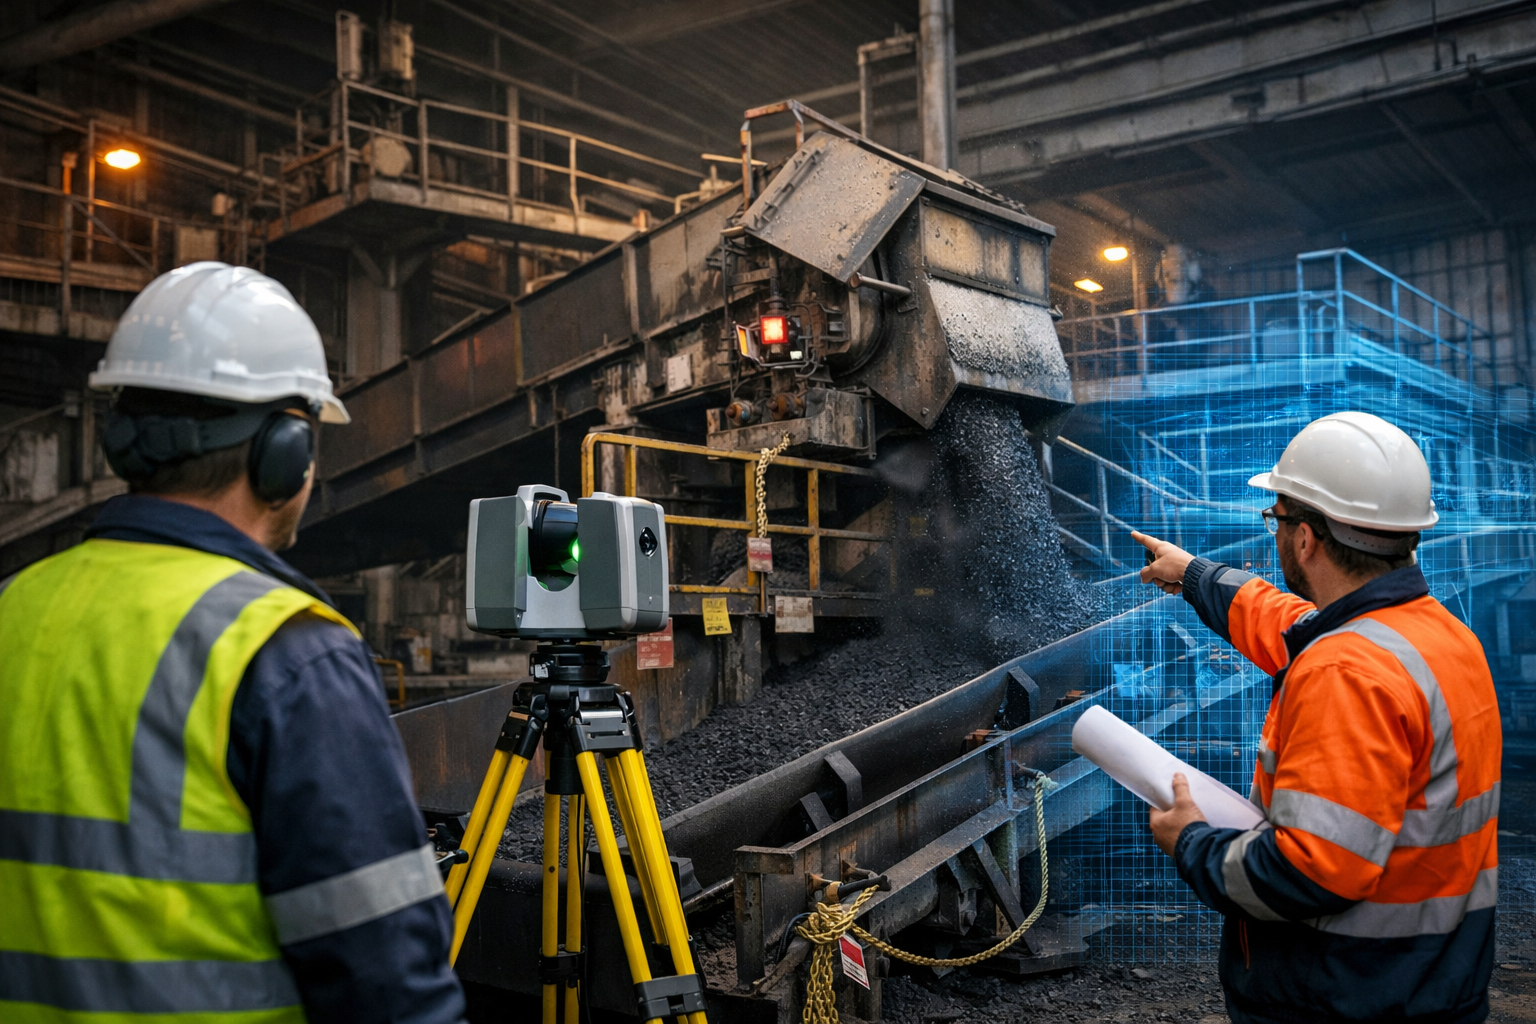
Our CHPP engineering services include existing-condition scanning, point-cloud registration, mechanical design, scan-to-CAD modelling, clash detection, general arrangements and fabrication drawings. We can also assist with equipment replacement, shutdown planning, chute modifications, conveyor upgrades and installation verification.
Combining mining experience with LiDAR scanning allows surrounding plant and connection points to be captured efficiently. The resulting point clouds and 3D models can help identify clearances, access requirements, structural interfaces and potential installation conflicts before fabrication begins.
Deliverables may include registered point clouds, 3D CAD models, general arrangement drawings, fabrication gra drawings and data suitable for AutoCAD, SolidWorks, Inventor, ReCap and Navisworks workflows.
Services are available across the Hunter Valley, Central Queensland and other coal-mining regions throughout Australia.
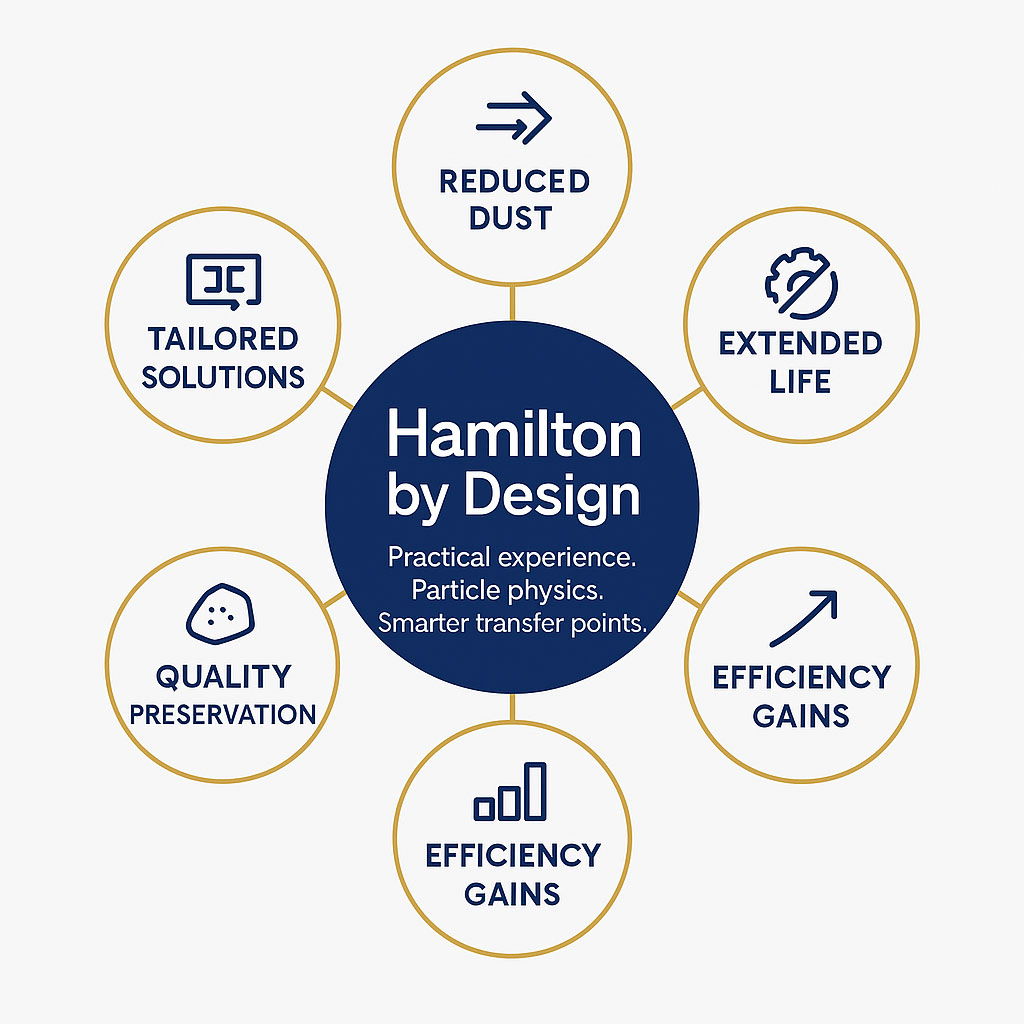
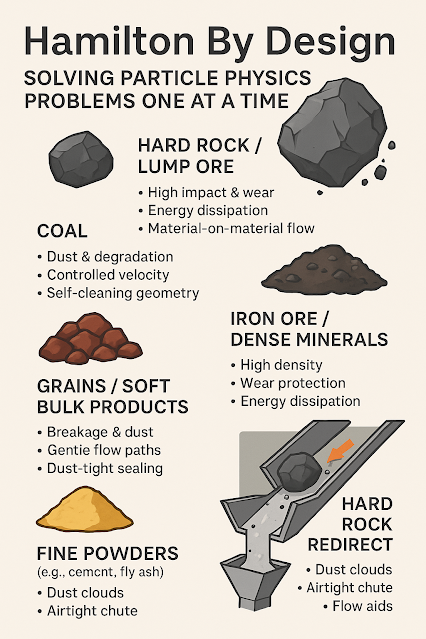
At Hamilton by Design, we see ourselves as more than engineers — we are problem-solvers who bring both science and experience to the table. Every bulk material transfer is unique, and each one carries its own challenges. By combining the principles of particle physics with decades of hands-on site experience, we design chutes and transfer points that perform in the real world, not just on a computer screen.
We are a small, specialised company, not a large corporate machine. That means you deal directly with the people who understand your operation, your materials, and your challenges. We take pride in our ability to stand on-site, watch the flow of material, and recognise behaviours that only years of experience can teach. This gives us the clarity to engineer practical solutions that keep your plant running reliably.
For us, your success is our success. We measure our achievement not by the number of projects we complete, but by the value we add to your operation — less dust, less wear, fewer stoppages, more tonnes moved.
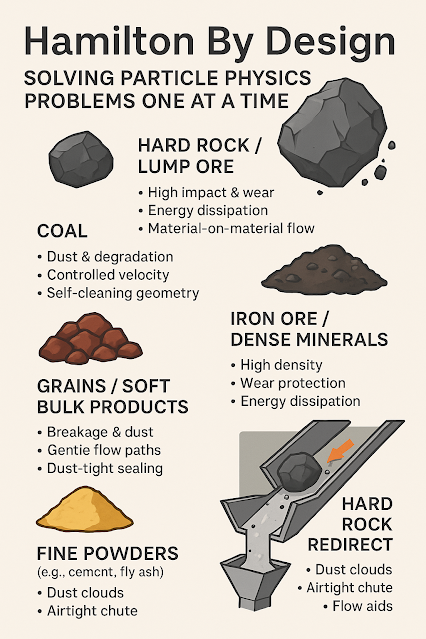
At Hamilton by Design, we believe that every bulk material transfer is an opportunity for improvement. What appears to be a simple flow of rock, coal, grain, or powder is, in reality, a particle physics problem waiting to be solved. By approaching these challenges with precision, creativity, and hands-on knowledge, we deliver chute designs that do more than move material — they protect assets, enhance performance, and improve the bottom line.
We are a small, specialised company with a wealth of on-site experience. Our engineers have spent years in the field, watching, listening, and learning how different materials behave under real conditions. This raw experience gives us a unique advantage: we can see and understand particle flow first-hand, not just through numbers on a screen. While many large organisations rely solely on computer models, we combine advanced simulation with practical insight, ensuring solutions that work not only in theory but also in practice.
Our team thrives on solving the complex problems others overlook:
Redirecting hard rock at speed without spillage or damage.
Handling sticky coal without blockages or hang-ups.
Containing fine powders without dust plumes or health risks.
Transferring fragile grains without breakage or product loss.
Extending chute, liner, and belt life with robust material-on-material flow designs.
We approach every challenge with the mindset that your success is our success. When your plant runs reliably, safely, and efficiently, we succeed alongside you. That’s why we design transfer points that:
Absorb and dissipate energy from high-impact lumps.
Control dust and minimise degradation for cleaner, safer operations.
Extend equipment life by reducing wear and maintenance.
Adapt to variability in feed size, flow, and moisture.
Boost throughput and availability by minimising stoppages.
In a world where margins are tight and environmental responsibility is critical, Hamilton by Design offers a personal, client-focused approach that puts performance and partnership at the centre. We are not a large organisation pushing generic solutions — we are a dedicated team that listens, observes, and engineers smarter outcomes, one particle physics problem at a time.
In the mining industry, system uptime isn’t just a goal—it’s a necessity. Transfer points such as chutes, hoppers, and conveyors are often the most failure-prone components in processing plants, especially in high-wear environments like HPGR (High Pressure Grinding Rolls) circuits. Abrasive ores, heavy impact, fines accumulation, and moisture can all combine to reduce flow efficiency, damage components, and drive up maintenance costs.
At Hamilton By Design, we help mining clients minimise downtime and extend the life of their material handling systems by applying advanced 3D scanning, DEM simulation, smart material selection, and modular design strategies. This ensures that transfer points operate at peak efficiency—day in, day out.
Here’s how we do it:
Optimised Flow with DEM-Based Chute & Hopper Design
Flow blockages and misaligned velocities are among the biggest contributors to transfer point failure in the mining industry. That’s why we use Discrete Element Method (DEM) simulations to model bulk material flow through chutes, hoppers, and transfer transitions.
Through DEM, we can simulate how different ores—ranging from dry coarse rock to sticky fines—move, compact, and impact structures. This allows us to tailor chute geometry, outlet angles, and flow paths in advance, helping:
Prevent material buildup or arching inside hoppers and chutes
Align material velocity with the conveyor belt speed using hood & spoon or trumpet-shaped designs
Reduce wear by managing trajectory and impact points
Not all wear is the same—and neither are the materials we use to combat it. By studying the abrasion and impact zones in your chute and hopper systems, we strategically apply wear liners suited to each application.
Our engineering team selects from:
AR (Abrasion-Resistant) steels for high-wear areas
Ceramic liners in fines-rich or ultra-abrasive streams
Rubber liners to absorb shock and reduce noise
This approach reduces liner replacement frequency, improves operational safety, and lowers the risk of unplanned shutdowns at key transfer points.
Dust and Spillage Control: Cleaner, Safer Operation
Dust and spillage around conveyors and transfer chutes can lead to extensive cleanup time, increased maintenance, and health hazards. At Hamilton By Design, we treat this as a core design challenge.
We design chutes and hoppers with:
Tight flange seals at interface points
Enclosed transitions that contain dust at the source
Controlled discharge points to reduce turbulent material drops
This reduces environmental risk and contributes to more consistent plant performance—especially in confined or enclosed processing facilities in the mining industry.
Modular & Accessible Designs for Faster Maintenance
When liners or components need replacement, every minute counts. That’s why our chute and hopper systems are built with modular sections—each engineered for fast removal and reinstallation.
Key maintenance-driven design features include:
Bolt-on panels or slide-in liner segments
Accessible inspection doors for safe visual checks
Lightweight modular components for easy handling
These details reduce labour time, enhance safety, and keep your plant online longer—especially critical in HPGR zones where throughput is non-stop.
Precision 3D Scanning & 3D Modelling for Retrofit Accuracy
One of the most powerful tools we use is 3D scanning. In retrofit or brownfield projects, physical measurements can be inaccurate or outdated. We solve this by conducting detailed laser scans that generate accurate point cloud data—a precise digital twin of your plant environment.
That data is then transformed into clean 3D CAD models, which we use to:
Design retrofits that precisely match existing structure
Identify interferences or fit-up clashes before fabrication
Reduce install time by ensuring right-first-time fits
This scan-to-CAD workflow dramatically reduces rework and error margins during installation, saving time and cost during shutdown windows.
Real-World Application: HPGR & Minerals Transfer Systems
In HPGR-based circuits, transfer points between crushers, screens, and conveyors experience high rates of wear, dust generation, and blockages—particularly where moisture-rich fines are present.
Here’s how Hamilton By Design’s methodology addresses these pain points:
DEM-based flow modelling ensures the HPGR discharge flows cleanly into chutes and onto conveyors without buildup.
Hood/spoon geometries help track material to belt velocity—minimising belt wear and reducing misalignment.
Strategic liner selection extends life in critical wear zones under extreme abrasion.
Modular chute designs allow for fast liner swap-outs without major disassembly.
3D scanning & CAD design ensures new chute sections fit seamlessly into existing HPGR and conveyor frameworks.
By designing smarter transfer systems with these technologies, we enable operators to reduce downtime, increase liner life, and protect critical assets in high-throughput mining applications.
Faster maintenance turnarounds during scheduled shutdowns
3D scanning & CAD integration
Precise fit, reduced installation time, fewer errors during retrofit
Final Word: Engineering That Keeps the Mining Industry Moving
At Hamilton By Design, we combine mechanical engineering expertise with 3D modelling, material flow simulation, and smart fabrication practices to deliver high-performance chute, hopper, and transfer point systems tailored for the mining industry.
Whether you’re dealing with a problematic HPGR discharge, spillage issues, or planning a brownfield upgrade, our integrated design process delivers results that improve reliability, extend service life, and protect uptime where it matters most.
Looking to retrofit or upgrade transfer systems at your site? Let’s talk. We bring together 3D scanning, DEM modelling, practical engineering, and proven reliability to deliver systems that work—from concept through to install.
Rigid Body Dynamics vs Transient Structural Analysis – How does it apply to the Mining industry?
In the Australian mining industry — where heavy equipment, high-value production, and harsh conditions are the norm — the ability to simulate, test, and validate mechanical systems before they are fabricated or fail in the field is not just beneficial, it’s essential.
From iron ore operations in the Pilbara, to gold mining east of Perth, across to coal in the Hunter Valley and Bowen Basin, and up to hard rock mines in Mount Isa, mining operations rely heavily on engineered systems that move, load, transfer, and endure extreme forces. These systems are increasingly modelled using computer-aided engineering (CAE) tools to improve design accuracy, increase reliability, and reduce downtime.
Two of the most powerful tools in the mechanical and structural engineering toolbox are Rigid Body Dynamics (RBD) and Transient Structural Analysis (TSA). Both play key roles — but they serve very different purposes.
At Hamilton By Design, we help clients across Australia choose and implement the right type of simulation, whether you’re evaluating motion, stress, fatigue, wear, or all of the above.
What is Transient Structural Analysis (TSA)?
Transient Structural Analysis is a finite element-based simulation used to evaluate how a structure deforms under time-dependent loads. It’s used to calculate:
Displacement and deformation
Internal stresses and strains
Vibrations and dynamic response
Fatigue or structural failure under repeated loading
TSA is essential for components subjected to impact, vibration, or varying loads over time — all of which are common in mining.
Mining Applications of TSA:
Vibrating screens and feeders
High-speed chutes or hoppers handling large volumes
Crusher housings and rotating equipment supports
Structural skids and frames under mobile loads
Transfer stations experiencing dynamic load shifts
What is Rigid Body Dynamics (RBD)?
Rigid Body Dynamics is used to simulate the motion of objects under the influence of forces, assuming the bodies themselves do not deform. RBD calculates:
Positions, velocities, and accelerations of components
Reaction forces at joints and constraints
Behaviour of actuators, linkages, and arms
Impact and collision between rigid parts
It’s particularly useful for modelling complex mechanisms and moving systems, such as hydraulic rams, rotary actuators, diverter gates, and articulated machinery.
Mining Applications of RBD:
Transfer chutes with moving diverter arms
Stacker-reclaimers and shiploaders
Drill mast articulation and boom operations
Hydraulic take-up systems on conveyors
Rockbreaker arms and crusher feed assemblies
Why TSA Isn’t a Substitute for RBD
Although TSA includes the ability to simulate rigid body motion as part of the total deformation field, it is not optimised for modelling systems where motion and kinematic behaviour are the primary focus. TSA solvers are geared towards tracking internal stresses, not joint movement or mechanical control.
If you try to use TSA for systems like diverter gates or mobile stackers:
The solver becomes slow and resource-heavy
You waste time calculating strain in components that are not expected to deform
You risk numerical instability if the system has insufficient structural constraints
RBD, on the other hand, is lean, fast, and perfectly suited for motion analysis. It handles joints, constraints, friction, impacts, and actuators efficiently without the complexity of a full finite element model.
Region-Specific Mining Examples
Let’s explore how these principles apply across key Australian mining regions.
🔶 Pilbara (Iron Ore – North of Perth)
In the Pilbara, high-throughput handling systems like stacker-reclaimers, conveyors, and train loadouts dominate. While TSA is critical for verifying the structural integrity of boom supports or transfer station bases, RBD is essential for simulating the precise motion of long booms, rotating car dumpers, and slewing mechanisms — especially when automated systems are involved.
🟡 Kalgoorlie & Goldfields (Gold – East of Perth)
In this region, we often see compact yet high-capacity systems like ball mills, crushers, and slurry pumps. TSA is ideal for evaluating fatigue life, support frame stresses, and dynamic loading from mill vibration. However, diverter systems in process plants or mobile material handling arms often require RBD to evaluate motion paths and ensure smooth operation under hydraulic or pneumatic control.
⚫ Hunter Valley (Thermal Coal)
Bulk handling is central in this region. TSA is used to assess the wear and fatigue life of chutes, hoppers, and vibrating feeders. For moving equipment like stackers, tripper cars, or sampler mechanisms, RBD provides fast, accurate insight into system dynamics, travel time, and constraint loads.
⚫ Bowen Basin (Metallurgical Coal)
Here, systems like longwall supports, draglines, and hydraulic roof supports dominate. RBD plays a crucial role in simulating the interaction between actuators and supports, ensuring control logic matches physical capability. TSA is then applied to determine structural integrity and fatigue under repetitive stress.
🔵 Mount Isa (Hard Rock Mining)
With aggressive ores and complex underground networks, Mount Isa operations demand robust systems. TSA is vital for verifying vibration resistance and structural life of crushers, vibrating screens, and bin supports. But the motion of equipment like rockbreakers, boom arms, and autonomous loaders must be analysed with RBD to ensure precise control and motion under harsh conditions.
Combining Both for Complete Insight
The real power comes when TSA and RBD are used together. For example:
Use RBD to simulate the motion of a diverter arm and identify peak reaction forces.
Feed those forces into a TSA model to evaluate stress and fatigue in the pivot brackets or mounting plates.
This combination provides full lifecycle analysis — motion, loads, stress, and safety.
Engineering Support from Hamilton By Design
At Hamilton By Design, we understand how to apply these tools to real-world mining problems. We specialise in:
Mechanical system simulation and analysis
Lidar scanning and digital plant modelling
Design for manufacturability and reliability
Integrated RBD + TSA solutions tailored to mining
Whether you’re developing a new materials handling system, upgrading an existing structure, or troubleshooting motion-related issues, our team can provide insight-driven solutions that save time and money.
👉 Learn more at www.hamiltonbydesign.com.au or contact us to request a capability statement or project discussion.
Final Thoughts
Rigid Body Dynamics and Transient Structural Analysis aren’t interchangeable — they are complementary. In the demanding environment of the mining industry, knowing when and how to use each tool can make the difference between a reliable plant and one plagued by maintenance issues and inefficiencies.
If your system moves, RBD gives you clarity. If it bends, vibrates, or wears, TSA gives you answers.
Hamilton By Design – Engineering Australia’s Mining Future.
🔧 Precision Engineering Meets Digital Innovation in the Mining Sector
In the heart of Australia’s mining country—Mount Isa—Hamilton By Design is delivering cutting-edge mechanical engineering solutions powered by 3D Lidar scanning and point cloud modelling.
Whether you’re managing underground infrastructure, fixed plant upgrades, or brownfield expansions, our advanced tools and design expertise help you visualise, optimise, and execute projects with clarity and confidence.
How We Support the Mining Industry
As mechanical engineering consultants, we provide services that reduce project risk, increase design accuracy, and streamline construction workflows. Key areas include:
Lidar 3D Scanning of existing plant, pipework, and underground assets
Point Cloud Creation for clash detection and design validation
Mechanical & Structural Drafting using accurate site data
Reverse Engineering of legacy plant or undocumented assets
Detailed Design for Modifications & Upgrades
Compliance, Auditing, and Risk Reduction
By combining field-tested mechanical engineering with cutting-edge digital capture, we help mining teams make better decisions—faster.
Why Mount Isa?
Mount Isa is home to some of Australia’s largest and most complex mining operations. From Glencore’s copper and zinc mines to contracting hubs servicing the broader North West Minerals Province, this region demands precision, speed, and deep mining knowledge.
Hamilton By Design is based locally in Mount Isa, giving us the unique advantage of rapid site access, practical experience in mining environments, and a strong understanding of local challenges.
Why Use Lidar & Point Clouds?
Lidar scanning has transformed how we approach engineering projects in mining:
Capture complex environments in minutes, not days
Generate ultra-accurate point clouds for design, measurement, and planning
Minimise rework by designing to exact, as-built geometry
Visualise site constraints in 3D before committing to fabrication or install
Integrate scan data with CAD models for seamless design workflows
From underground crushers to surface pipe racks, our Lidar system captures the details—so you can design with certainty.
Use Cases in Mining Projects
Some real-world examples of how we apply mechanical engineering + Lidar scanning in mining:
Scanning underground pump stations for upgrade design
Reverse-engineering chutes and hoppers with no existing drawings
Capturing point clouds of processing plants for structural fit-out
Laser-accurate data for mobile plant modifications and safety guarding
Converting scan data into fabrication-ready models and drawings
Want to see a sample point cloud or project output? Just reach out through our website below.
Who We Work With
Mining Operators & Engineers
Shutdown Coordinators
Project Managers & Fabricators
EPCM Contractors
Surveyors & Design Teams
If you’re responsible for delivering accurate, efficient, and safe mechanical solutions on site—Hamilton By Design is your local partner.
Operation, Design Challenges, and the Role of Direct Drive Units In the highly demanding and regulated world of underground coal mining, the reliable and efficient transport of coal from the mining face to the surface is critical. Among the many systems involved in this process, conveyor drives play a pivotal role. These systems are tasked with powering conveyor belts that haul coal over long distances through often confined and hazardous environments. A vital part of this setup includes the use of direct drive units (DDUs), particularly in low-profile applications such as underground operations.
This document explores the functionality of conveyor drives in underground coal mines, the unique challenges faced in their operation, the complexities design engineers encounter in their development, and the concept of the phase “outbye”—a term widely used in underground mining to describe the direction and location of operations.
Conveyor Drives in Underground Coal Mining
A conveyor drive is a mechanical system that powers conveyor belts used to transport materials, in this case, coal. In underground mines, these conveyor belts often run for several kilometers, extending from the coal face (the area where coal is actively being cut and mined) to the shaft or drift that brings the coal to the surface.
The drive systems can be located at several points along the belt:
Head drive: Located at the discharge end of the conveyor.
Tail drive: Located at the loading end.
Mid-belt drives: Installed partway along long conveyors to help manage torque and reduce belt tension.
In the context of underground coal mines, the term “conveyor drive” is generally associated with the head or tail drive unit, which powers the movement of the belt.
Role of Direct Drive Units (DDUs)
Direct Drive Units are electric motors directly coupled to the drive shaft of the conveyor pulley, eliminating the need for intermediary gearboxes or belt drives. These units are especially advantageous in underground mining due to their compact design, reliability, and reduced maintenance.
Benefits of DDUs in Underground Coal Mines
Compact Size: Ideal for low-profile mining applications where vertical space is restricted.
Energy Efficiency: With fewer mechanical components, DDUs offer less friction and mechanical losses.
Lower Maintenance: No gearboxes or belt couplings to service.
Increased Reliability: Fewer parts mean fewer failure points.
Improved Safety: The enclosed design minimizes exposure to moving parts and flammable materials.
Operational Challenges of Conveyor Drives Underground
Underground coal mining presents a set of challenges not commonly encountered in surface operations. Conveyor drives, as the lifeblood of coal transportation, are central to these operational difficulties.
1. Space Constraints
Underground roadways are typically narrow and low, especially in coal seams with minimal thickness. This limitation forces the use of low-profile conveyor systems, which in turn limits the size and configuration of the drive units.
2. Dust and Moisture Exposure
Coal dust is highly abrasive and, in certain concentrations, explosive. Moisture from groundwater or the mining process further complicates the reliability of drive components. Ensuring DDUs are properly sealed and rated for these harsh conditions is critical.
3. Heat and Ventilation
Electric motors generate heat, which must be dissipated. However, underground mines have limited ventilation. Overheating can be a major issue, requiring cooling systems or specialized motor enclosures.
4. Explosion-Proof Requirements
Due to the potential presence of methane gas and coal dust, all electrical equipment, including conveyor drives, must comply with stringent explosion-proof standards (e.g., IECEx or ATEX ratings).
5. Long Haul Distances
Modern coal faces can be several kilometers from the shaft bottom. Transporting coal over long distances places mechanical stress on conveyor belts and drive units, increasing the risk of failure if not properly engineered.
6. Maintenance Access
Accessing conveyor drives for inspection or maintenance can be difficult in tight underground environments. Failures that require replacement or repair can cause significant production delays.
7. Load Variability
The volume of coal being hauled can vary significantly during a shift, which places variable demands on the drive system. The control systems must be able to accommodate fluctuating loads without mechanical strain.
Engineering and Design Challenges
Design engineers are tasked with creating conveyor drive systems that are not only robust and efficient but also compact and compliant with mining regulations. Some of the key design challenges include:
1. System Integration in Confined Spaces
Engineering a system that fits into limited space while delivering the necessary power is a fundamental challenge. Direct drive units help address this by eliminating gearboxes, but the motor itself must still be sized correctly.
2. Material Selection
Materials used must be corrosion-resistant, non-sparking, and capable of withstanding vibration, dust ingress, and moisture. This often limits design options and increases costs.
3. Thermal Management
Ensuring that the drive units do not overheat requires careful thermal modeling and the use of heat-resistant components. In some cases, passive or active cooling systems are integrated.
4. Compliance with Standards
Designs must adhere to a host of mining and electrical standards for flameproof and intrinsically safe equipment. Certification processes can be lengthy and expensive.
5. Modularity and Transportability
Since access to underground sites is limited, equipment must be modular or transportable in pieces small enough to be moved through shafts or drifts. Assembling and commissioning underground adds another layer of complexity.
6. System Control and Monitoring
Advanced drives require smart control systems that can adjust to load demands, monitor for faults, and integrate with mine-wide automation systems. Designing these systems requires interdisciplinary expertise.
7. Redundancy and Reliability Engineering
System failure underground can halt production and pose safety risks. Engineers must design for redundancy and easy switch-over between drive systems when necessary.
Understanding the Term “Outbye”
In underground mining terminology, directionality is essential for communication and logistics. The terms “inbye” and “outbye” are commonly used to describe relative directions underground.
What Does “Outbye” Mean?
Outbye refers to the direction away from the coal face and toward the surface or the mine entrance.
Conversely, inbye means toward the coal face.
For example:
If a miner is walking from the coal face toward the conveyor belt transfer station, they are walking outbye.
If a service vehicle is heading toward the longwall face, it is moving inbye.
Relevance of “Outbye” in Conveyor Systems
In conveyor operations:
The coal face is the inbye starting point.
The belt head drive and transfer points to the main conveyor system are located outbye.
Maintenance and service activities often take place outbye to avoid interfering with production at the face.
Understanding this term is critical for coordinating activities underground, as directions are often communicated using inbye and outbye references rather than compass points or distances.
Innovations and Future Trends
The mining industry continues to evolve, and conveyor drive systems are no exception. Some of the emerging trends and technologies include:
1. Variable Speed Drives (VSDs)
VSDs allow precise control over motor speed and torque, improving efficiency and reducing mechanical stress. They are increasingly paired with direct drive units to optimize performance.
2. Condition Monitoring
Sensors embedded in motors and drive systems can provide real-time feedback on vibration, temperature, and load. Predictive maintenance models reduce downtime.
3. Permanent Magnet Motors
These motors offer higher efficiency and torque density compared to traditional induction motors, making them well-suited for space-constrained environments.
4. Automation and Remote Control
Fully integrated systems that allow operators to monitor and control conveyor drives from surface control rooms are becoming standard.
5. Modular, Plug-and-Play Designs
Future drive units are being designed with ease of installation and replacement in mind, enabling faster deployment and lower maintenance impact.
Conclusion
Conveyor drive systems in underground coal mining are vital to the continuous flow of material and, by extension, the productivity of the entire mining operation. The adoption of direct drive units is helping to meet the unique demands of underground environments by providing compact, reliable, and efficient power transmission solutions.
However, these systems are not without their challenges. From the operational constraints of underground environments to the rigorous demands placed on design engineers, the development and maintenance of these systems require specialized knowledge, innovative thinking, and strict adherence to safety standards.
Moreover, understanding mining-specific terminology such as “outbye” provides important context for the deployment and maintenance of conveyor systems. As technology continues to advance, we can expect to see more intelligent, adaptive, and efficient conveyor drive systems that are better suited to the evolving demands of underground coal mining.
To provide the best experiences, we use technologies like cookies to store and/or access device information. Consenting to these technologies will allow us to process data such as browsing behaviour or unique IDs on this site. Not consenting or withdrawing consent, may adversely affect certain features and functions.
Functional
Always active
The technical storage or access is strictly necessary for the legitimate purpose of enabling the use of a specific service explicitly requested by the subscriber or user, or for the sole purpose of carrying out the transmission of a communication over an electronic communications network.
Preferences
The technical storage or access is necessary for the legitimate purpose of storing preferences that are not requested by the subscriber or user.
Statistics
The technical storage or access that is used exclusively for statistical purposes.The technical storage or access that is used exclusively for anonymous statistical purposes. Without a subpoena, voluntary compliance on the part of your Internet Service Provider, or additional records from a third party, information stored or retrieved for this purpose alone cannot usually be used to identify you.
Marketing
The technical storage or access is required to create user profiles to send advertising, or to track the user on a website or across several websites for similar marketing purposes.