Understanding Mining Equipment Wear

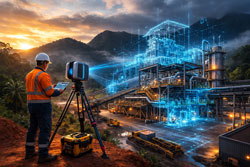
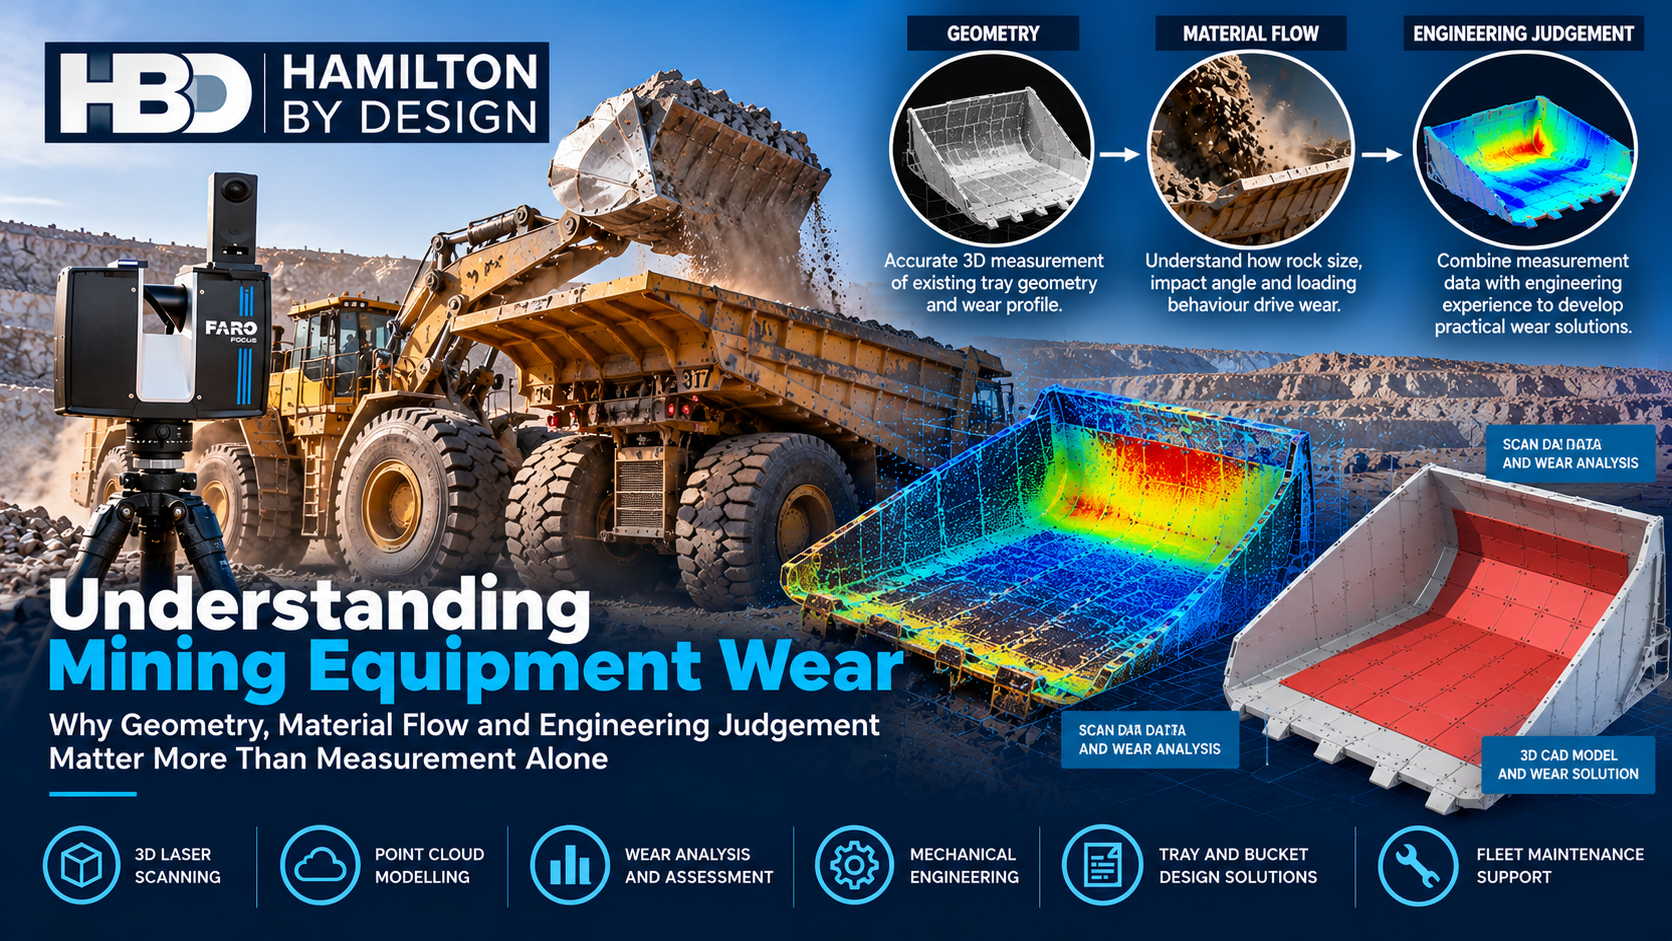
3D LiDAR scanning of mining haul truck tray and wheel loader bucket wear using a FARO Focus scanner, showing point cloud modelling, wear analysis and mechanical engineering by Hamilton By Design.

Are We Measuring Wear or Understanding It?

Understanding Mining Equipment Wear โ€“ Why Geometry, Material Flow and Engineering Judgement Matter More Than Measurement Alone

Today’s engineers have access to an exceptional range of measurement technologies.

Blue 3D LiDAR scanner icon on a tripod with scanning waves

3D LiDAR scanning, ultrasonic thickness testing, laser metrology, photogrammetry, vibration analysis and advanced CAD modelling allow equipment condition to be assessed with considerable detail.

However, at Hamilton By Design, we believe there is an important distinction between measuring wear and understanding why wear occurs.

A surveyor may identify a 15 mm variation in the geometry of a truck tray. A maintenance engineer may identify repeated wear plate replacement. A reliability engineer may establish that equipment service life is declining.

All three observations are valuable, but none necessarily explains why material is contacting a particular surface, why a component is deforming or whether a change in geometry could reduce the problem.

We consider that effective wear assessment requires a combination of accurate measurement, mechanical engineering, material-flow understanding and practical operating experience.

This philosophy also relates to our article on Project Management Challenges, where accurate existing-condition information and well-defined engineering requirements are important considerations.

1. Why Loader Buckets and Haul Truck Trays Experience Different Wear

Although loader buckets and haul truck trays handle similar materials, their operating conditions are fundamentally different.

A loader bucket penetrates and displaces material. Its cutting edge, teeth and protective components experience substantial digging forces, contact pressure, gouging and abrasive sliding.

A haul truck tray receives material, transports it and subsequently discharges it under gravity.

Wear considerationLoader bucketHaul truck tray
Ground engagementHigh during diggingGenerally none
Abrasive contactDigging and material movementLoading and discharge
Impact loadingDigging and fillingMaterial falling into tray
Material throughputCombined production of multiple trucksIndividual truck production
Wear protectionTeeth, cutting edges, shrouds and linersFloor liners, impact protection and wear plates
Main design considerationDigging efficiency and durabilityPayload efficiency and structural durability

Loader buckets commonly incorporate extensive replaceable wear protection because their ground-engaging surfaces experience severe abrasive contact.

However, this does not automatically mean the loader bucket structure will wear out before the truck tray.

2. Operating Cycles โ€“ One Loader Servicing Multiple Trucks

A common mistake when comparing wear is to assume that one loader operates with one truck.

In reality, a loader may service several haul trucks.

Consider the following hypothetical mining operation.

Operating parameterAssumed value
Number of loaders1
Number of haul trucks5
Truck payload120 tonnes
Effective bucket payload20 tonnes
Bucket passes per truck6
Complete truck cycle30 minutes
Operating hours per day20
Operating days per year300

The truck cycle includes loading, hauling, tipping and returning. The example assumes sufficient loading capacity and no significant operational delays.

Calculation 1 โ€“ Truck Cycles

Each truck completes:

40 loads/day = (20 ร— 60) รท 30

Across five trucks:

5 ร— 40 = 200 truckloads/day

Calculation 2 โ€“ Daily Material Throughput

200 ร— 120 = 24,000 tonnes/day

Each individual truck carries:

40 ร— 120 = 4,800 tonnes/day

The loader therefore handles five times the material throughput of an individual truck tray.

Calculation 3 โ€“ Loader Bucket Cycles

Each truck requires six bucket passes.

200 ร— 6 = 1,200 bucket cycles/day

Each individual truck tray receives:

40 ร— 6 = 240 bucket discharge events/day

Annual Operating Exposure

ParameterLoader bucketIndividual truck tray
Daily throughput24,000 tonnes4,800 tonnes
Annual throughput7,200,000 tonnes1,440,000 tonnes
Daily material-handling events1,200240
Annual material-handling events360,00072,000

The loader experiences five times the material throughput and material-handling events of an individual truck tray.

However, five times the throughput does not necessarily mean five times the wear.

The actual wear rate depends on material characteristics, contact pressure, particle movement, impact conditions and wear protection.

Operating Capacity and Haul Cycle Assumptions

The production calculations presented are based on a simplified mining fleet consisting of one wheel loader servicing five haul trucks, each with a payload of 120 tonnes.

The assumed 30-minute haul truck cycle includes loading, loaded travel, dumping, empty return travel and associated delays.

Actual cycle times depend on haul distance, road conditions, gradients, travel speeds, loading efficiency and equipment availability.

A shorter haul distance may increase the number of truckloads completed per shift, while a longer haul distance may reduce the frequency of loading and unloading events.

The loader must also have sufficient capacity to service the trucks at the required rate without becoming a production bottleneck.

These operating conditions directly influence the cumulative tonnes handled and the number of loading and unloading cycles experienced by each machine.

Consequently, wear exposure should be assessed using actual operating hours, material throughput, loading cycles and equipment geometry rather than operating time alone.

The calculations are illustrative and are not intended to represent the production performance of a particular mining operation.

3. Particle Size โ€“ Is It Controlled by the Production Process?

Particle-size distribution is an important factor in equipment wear.

In conventional open-pit mining, loaders and haul trucks often handle run-of-mine material before primary crushing.

Although drilling and blasting influence fragmentation, particle sizes may vary considerably.

In downstream processing operations, crushing and screening generally provide greater control over particle-size distribution.

Particle conditionPotential wear mechanism
Fine hard particlesAbrasive sliding and scratching
Medium angular particlesCutting and gouging
Large rock fragmentsLocalised impact and deformation
Oversize materialHigh impact forces and potential structural damage
Wet or cohesive materialMaterial buildup and altered flow behaviour

Material hardness, particle shape, density and moisture content also influence wear.

A large angular rock may create significant localised impact damage, while smaller hard particles can produce substantial abrasive wear under sustained contact pressure.

Therefore, particle size alone cannot predict wear performance.

4. The Cutting Tool Principle โ€“ Can Geometry Reduce Wear?

At Hamilton By Design, we consider that wear protection should not simply involve selecting harder steel or installing thicker wear liners.

An important design consideration is whether equipment geometry can reduce unnecessary abrasive contact.

A useful comparison can be made with cutting tools used on milling machines and lathes.

Cutting tools incorporate clearance or relief angles behind the cutting edge.

These angles reduce unnecessary rubbing between the tool and the newly machined surface.

The cutting edge performs the intended work, while the geometry behind it reduces unwanted contact.

We consider that this general design principle has relevance to bulk material handling equipment.

Loader Buckets

A loader bucket must penetrate material during digging.

However, the geometry of the cutting edge, heel, side protection and external wear components influences which surfaces experience abrasive contact.

Appropriate relief geometry and wear protection may reduce unnecessary rubbing and protect the main bucket structure.

Truck Trays, Hoppers and Transfer Chutes

The same broad principle can be considered when designing truck trays, hoppers and transfer chutes.

Where material trajectories can be controlled to reduce unnecessary contact with surrounding surfaces, localised abrasive wear may be reduced.

However, loose rock does not behave like a workpiece on a lathe.

Particles can rotate, rebound, collide and change direction.

Increasing clearance without considering the complete material-flow path may transfer wear to another location or increase impact severity.

The engineering objective should therefore be to establish suitable geometry and material movement rather than simply maximise clearance.

5. Vertical Ore Passes โ€“ Understanding Material Movement and Wear

Vertical and steeply inclined ore passes provide an interesting example of the relationship between geometry, movement and wear.

In underground mining, fragmented rock may be transferred between levels through gravity-fed ore passes.

Where material travels through a vertical section without continuous wall contact, abrasive sliding along those surfaces may be reduced.

However, this does not eliminate wear.

Material may strike the walls, rebound, change direction or impact receiving structures.

Calculation 4 โ€“ Gravitational Potential Energy

The gravitational potential energy of falling material is:

E = m ร— g ร— h

Where:

  • E = gravitational potential energy (joules)
  • m = material mass (kg)
  • g = gravitational acceleration (9.81 m/sยฒ)
  • h = vertical drop height (m)

Consider a 100 kg rock falling through 10 metres.

E = 100 ร— 9.81 ร— 10

E = 9,810 J = 9.81 kJ

For a 30-metre drop:

E = 100 ร— 9.81 ร— 30

E = 29,430 J = 29.43 kJ

Vertical dropPotential energy
5 m4.91 kJ
10 m9.81 kJ
20 m19.62 kJ
30 m29.43 kJ

These calculations illustrate the increase in gravitational potential energy with drop height. They do not establish the energy actually absorbed by a particular surface.

The actual impact conditions depend on particle trajectory, collisions, energy losses and contact geometry.

Reducing wall contact in one section of an ore pass may reduce abrasion there, while concentrating impact damage at another location.

For this reason, the entire material-flow path must be considered.

6. Surveying Measures Variation โ€“ Engineering Must Understand Wear

Modern surveying technologies allow engineers and surveyors to identify geometric differences with considerable accuracy.

However, a measured variation does not necessarily establish the mechanism responsible for that variation.

A surveyor may report that a truck tray floor has deviated by 15 mm from a reference model.

From a surveying perspective, this is a measurable geometric difference.

From a mechanical engineering perspective, several questions remain.

Has the steel worn away? Has the plate permanently deformed? Was the original geometry different from the reference? Has the structure moved under load?

Measured conditionPossible engineering explanation
15 mm truck tray floor deviationWear, deformation or original geometry
10 mm chute wall displacementStructural movement, damage or installation variation
8 mm bucket cutting-edge reductionPotential abrasive material loss
Ore pass wall irregularityExcavation geometry, impact or wear
Reduced operating clearanceDeflection, movement or misalignment

Surveyors provide valuable expertise in dimensional measurement, spatial relationships and geometric accuracy.

However, surveying expertise does not automatically include specialist knowledge of tribology, mechanical wear, material flow or structural behaviour.

Equally, mechanical engineers depend on reliable dimensional information to make defensible engineering decisions.

At Hamilton By Design, we consider these disciplines complementary.

Surveying establishes the geometry. Engineering interpretation establishes what that geometry means for equipment performance.

This is closely related to our article Why Engineers, Designers & Project Managers Are Turning to 3D Scanning and CAD Modelling.

7. Static Geometry Is Not the Same as Operating Geometry

A 3D scan generally captures equipment geometry at a particular moment.

However, equipment may move or deform under operating loads.

A static measurement does not automatically establish the minimum clearance available throughout the operating cycle.

Consider the following simplified example.

ParameterValue
Initial static clearance50 mm
Component A movement towards B20 mm
Component B movement towards A15 mm

Remaining clearance:

50 โˆ’ 20 โˆ’ 15 = 15 mm

The original 50 mm clearance has reduced to 15 mm under the assumed operating conditions.

Actual assessments must consider movement direction, load cases, thermal effects, tolerances and dynamic behaviour.

This illustrates why accurate measurement of stationary equipment is only one part of understanding its operating geometry.

A component may be manufactured and installed accurately yet experience excessive wear because its movement or material-flow conditions have not been adequately considered.

8. Modern Wear Measurement Technologies

Different technologies answer different engineering questions.

TechnologyPrimary application
3D LiDAR scanningLarge-scale geometry and deformation comparison
Metrology scanningDetailed component geometry
Ultrasonic thickness testingRemaining steel plate thickness
Vibration analysisRotating equipment condition and dynamic behaviour
CAD modellingGeometry, clearance and modification design
Finite Element AnalysisStructural response under defined loads
Material-flow simulationParticle trajectories and contact behaviour

No single technology provides every answer.

For example, 3D LiDAR scanning measures visible surface geometry but does not directly establish remaining steel thickness.

Ultrasonic thickness testing can measure remaining plate thickness at suitable locations but does not establish the complete three-dimensional deformation of a truck tray.

The appropriate measurement approach depends on the engineering objective.

9. Connecting Wear Assessment with Condition-Based Maintenance

Wear assessment is closely related to maintenance strategy.

Hamilton By Design discusses maintenance approaches in our article ISO 18436-2 Maintenance Strategies.

ISO 18436-2 addresses qualification and assessment of personnel involved in vibration condition monitoring and diagnostics. It is not a truck tray wear assessment standard.

Nevertheless, the broader principles of condition monitoring, repeated inspection and reliability engineering are relevant to managing wear.

Calculation 5 โ€“ Establishing a Wear Rate

Assume a steel wear liner has the following measured thicknesses.

ParameterValue
Initial thickness20 mm
Remaining thickness16 mm
Operating period1,000 hours
Assumed minimum allowable thickness10 mm

Material loss:

20 โˆ’ 16 = 4 mm

Average wear rate:

4 รท 1,000 = 0.004 mm/hour

Equivalent to:

4 mm per 1,000 operating hours

If the wear rate remained constant, the estimated time to reach the assumed minimum thickness would be:

(16 โˆ’ 10) รท 0.004

Estimated remaining operating time = 1,500 hours

This is a simplified linear projection, not a verified remaining-life prediction.

Actual wear may accelerate or reduce as operating conditions, material characteristics and component geometry change.

The minimum allowable thickness must also be established through an appropriate engineering assessment.

10. From Measurement to 3D Modelling and Engineering Improvement

3D scanning and modelling provide opportunities to move beyond documenting existing equipment condition.

Our article 3D Modelling with You Now and 3D Modelling in the Future discusses the importance of digital engineering models and their application to design development.

For wear investigations, a practical workflow may include:

  1. Establish the wear or deformation problem.
  2. Capture existing geometry using suitable measurement methods.
  3. Obtain thickness measurements and other inspection information where required.
  4. Establish reference geometry from OEM drawings, historical scans or CAD models.
  5. Review material properties, operating cycles and equipment movement.
  6. Develop a 3D model of the equipment.
  7. Investigate material trajectories, clearances and possible modifications.
  8. Undertake appropriate engineering calculations or analysis.
  9. Develop replacement components or modification drawings.
  10. Monitor equipment performance following implementation.

This approach allows the engineering assessment to investigate not only what has changed but also why it has changed.

11. Why Every Wear Assessment Project Is Different

At Hamilton By Design, we recognise that every project is different, and no single wear assessment methodology should automatically be applied to all equipment.

Even two truck trays supplied by the same manufacturer may experience substantially different wear patterns.

Differences may result from:

  • Material hardness and particle-size distribution.
  • Loading height and impact conditions.
  • Material throughput and operating cycles.
  • Wear liner materials and configurations.
  • Equipment geometry and movement.
  • Previous repairs and maintenance.
  • Material moisture and flow behaviour.
  • Inspection history and available reference information.

A project intended to measure geometric deformation may require different inspection methods and deliverables from one investigating remaining plate thickness or structural fatigue.

Similarly, a transfer chute experiencing repeated liner failure may require an investigation of material trajectory rather than simply increasing wear liner thickness.

An engineering report prepared for one project should not automatically be considered representative of another.

The scope, methodology, calculations and deliverables should be developed around the actual equipment, operating conditions and engineering outcomes required.

12. Why Project Management Matters

Wear assessment is not only a technical challenge. It is also a project management consideration.

Poorly defined scopes, incomplete reference information and uncertainty about deliverables can lead to unnecessary work, delays and additional costs.

Our article Project Management Challenges discusses the importance of accurate information, planning and clear engineering requirements.

Before commencing a wear investigation, the client and engineering team should establish whether the objective is to:

  • Measure existing material loss.
  • Assess deformation.
  • Determine remaining serviceability.
  • Investigate recurring wear failures.
  • Develop replacement wear protection.
  • Modify equipment geometry.
  • Improve maintenance planning.

These objectives may require different engineering disciplines, inspection methods, calculations and reporting arrangements.

13. Hamilton By Design โ€“ Our Engineering Approach

Hamilton By Design provides mechanical engineering, 3D LiDAR scanning, reverse engineering and CAD modelling services for mining and industrial equipment.

Our approach considers the relationship between measured geometry, material characteristics and equipment operation.

We recognise that accurate measurement is essential, but the value of that information depends on how it is interpreted and applied.

For equipment such as loader buckets, haul truck trays, transfer chutes, hoppers and underground ore passes, an effective assessment may involve understanding material flow, identifying unnecessary contact, reviewing wear protection and investigating geometric improvements.

We believe the appropriate solution is not always to install thicker steel or harder wear liners.

In some applications, improvements to geometry, clearance, material trajectory or maintenance strategy may offer greater long-term benefits.

However, any proposed modification must be assessed against the equipment’s actual operating conditions, structural requirements and intended function.

Conclusion โ€“ Measuring Wear Is Only the Beginning

Today’s engineers have access to sophisticated technologies for measuring wear, deformation and equipment condition.

However, the ability to measure a geometric variation does not necessarily establish the cause of that variation.

A surveyor may identify where a component differs from its reference geometry. An inspection specialist may establish remaining plate thickness. A reliability engineer may identify recurring failures.

Mechanical engineering assessment brings these findings together with material behaviour, equipment geometry, operating movement and structural requirements.

The distinction is important.

A loader bucket may handle the combined material throughput of several haul trucks, but this does not automatically establish its relative wear rate.

A truck tray may experience fewer material-handling events but still suffer severe impact damage.

A vertical ore pass may experience reduced wall abrasion in one section while concentrating impact damage elsewhere.

A transfer chute may repeatedly wear through its liners because of an unfavourable material trajectory rather than insufficient liner hardness.

At Hamilton By Design, we believe the engineering objective should extend beyond measuring how much material has been lost. We should investigate why it was lost, whether unnecessary contact can be reduced and how equipment performance can be improved.

Every project is different.

The most appropriate assessment is one developed around the actual equipment, its operating conditions, the available evidence and the engineering outcomes required.

Measurement identifies the condition. Engineering explains the mechanism. Good design addresses the cause.


Project Management Challenges

The importance of accurate existing-condition information, scope definition, engineering workflows and project planning.

ISO 18436-2 Maintenance Strategies

Condition monitoring, reliability engineering and maintenance approaches.

3D Modelling with You Now and 3D Modelling in the Future

Using 3D modelling and digital engineering to support equipment design and modification.

Why Engineers, Designers & Project Managers Are Turning to 3D Scanning and CAD Modelling

Capturing existing geometry and converting it into practical engineering models and drawings.


Hamilton By Design

Mechanical Engineering | 3D LiDAR Scanning | Reverse Engineering | 3D Modelling

Website: https://www.hamiltonbydesign.com.au/

Engineering calculations in this article are illustrative examples only. They do not represent verified equipment performance data or substitute for project-specific engineering assessment.

Hamilton By Design logo displayed on a blue tilted rectangle with a grey gradient background

Contact Us – Talk To Us

Name
Would you like us to arrange a phone consultation for you?
Address

Our clients:


Conveyor Reliability Matters

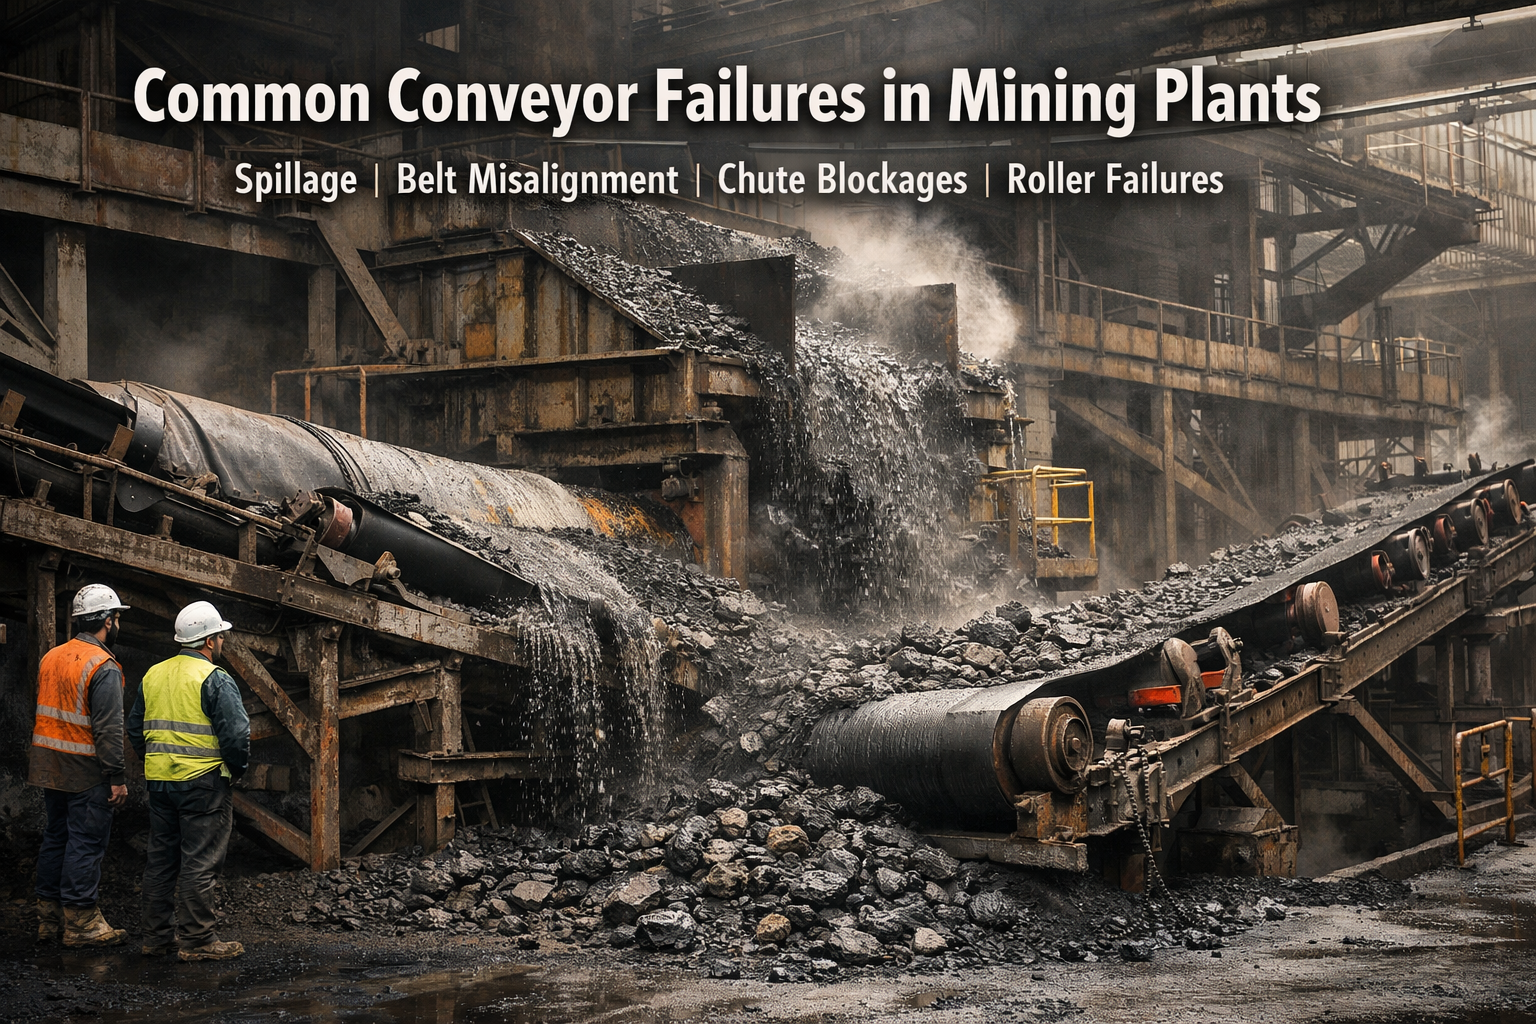
Conveyor system failure in a mining processing plant with spillage and damaged rollers.

Conveyor systems are the backbone of most mining operations. They move thousands of tonnes of ore every hour between crushers, processing plants, stockpiles, and load-out facilities.

When a conveyor fails, the impact can be immediate and costly. Production stops, plant operators must respond quickly, and maintenance teams are forced to work under pressure to restore operations.

Understanding the common causes of conveyor failures in mining plants is essential for improving plant reliability and reducing unplanned downtime.


1. Conveyor Belt Damage

One of the most frequent conveyor failures in mining is damage to the conveyor belt itself.

Typical causes include:

  • impact from large rocks at transfer points
  • sharp materials cutting the belt
  • misaligned loading onto the receiving belt
  • worn or damaged idlers

When belts become damaged, operations may experience:

  • belt tears
  • belt mistracking
  • material spillage

Over time this leads to reduced production efficiency and increased maintenance costs.

Proper chute design and impact control can significantly reduce belt damage.


2. Transfer Chute Blockages

Transfer chutes are often the most problematic areas in materials handling systems.

Poorly designed transfer chutes can cause:

  • material build-up
  • flow restrictions
  • complete blockages

These problems are especially common when handling:

  • wet ore
  • sticky materials
  • fine particles

When chutes block, the upstream conveyors continue feeding material until the system trips or operators intervene.

This can quickly escalate into major plant disruptions.


3. Conveyor Misalignment

Another common maintenance issue is belt misalignment.

Misalignment occurs when the belt does not track correctly along the conveyor structure.

Common causes include:

  • uneven loading at transfer points
  • worn idlers
  • structural movement or damage
  • incorrect installation

When conveyors run out of alignment they can cause:

  • edge damage to belts
  • excessive wear on idlers
  • safety hazards from material spillage

Regular inspection and proper transfer design can reduce this risk.


4. Structural Fatigue and Failure

Mining conveyors operate in harsh environments and are subjected to constant vibration and loading.

Over time this can lead to structural issues such as:

  • cracked steel structures
  • damaged conveyor supports
  • fatigue in transfer chute frames

These failures may not be immediately visible but can develop gradually over years of operation.

Engineering inspections and accurate plant modelling can help identify these risks before they become critical failures.


5. Wear in Materials Handling Equipment

Mining materials are often highly abrasive.

Components that commonly experience heavy wear include:

  • chute liners
  • skirt plates
  • idlers
  • pulley lagging

If these parts are not replaced in time, they can lead to larger system failures.

Preventative maintenance programs help ensure that wear components are replaced before reliability issues develop.


Improving Plant Reliability Through Engineering

Reducing conveyor failures in mining plants requires a combination of:

  • good engineering design
  • proper maintenance practices
  • accurate understanding of existing plant infrastructure

Modern engineering techniques such as 3D laser scanning and digital modelling allow engineers to capture the true geometry of operating plants.

This helps identify problems such as:

  • poor transfer geometry
  • structural clashes
  • restricted maintenance access

These issues can then be addressed before they lead to operational failures.

You can learn more about mining mechanical engineering design services here:


Preparing Conveyor Upgrades During Shutdowns

Many conveyor upgrades and maintenance projects are performed during planned plant shutdowns.

Because shutdown windows are limited, careful preparation is essential.

Engineering preparation may include:

  • capturing existing plant conditions
  • producing detailed engineering models
  • planning structural modifications
  • preparing fabrication drawings

Proper shutdown planning reduces the risk of installation delays and ensures that maintenance work is completed safely.

Learn more about shutdown preparation here:


Using Digital Engineering to Reduce Risk

Digital engineering tools now allow mining operations to develop accurate digital models of their processing plants.

These models help engineers:

  • analyse conveyor systems
  • redesign transfer chutes
  • identify potential failure points
  • plan upgrades with confidence

By using digital engineering models, mining companies can significantly reduce the risk of plant downtime and improve overall reliability.

More information on this approach can be found here:


Final Thoughts

Conveyor systems are critical to the performance of mining plants, but they are also one of the most common sources of operational failure.

By understanding the causes of conveyor failures in mining, operations teams can focus on improving:

  • transfer chute design
  • maintenance practices
  • plant engineering preparation

Through proper engineering and planning, mining companies can improve reliability, reduce downtime, and ensure that their materials handling systems continue to operate safely and efficiently.

3D LiDAR scanning and 3D modelling service button โ€” laser scanner capturing a point cloud for engineering and CAD modelling
Mechanical engineering services
Name
Would you like us to arrange a phone consultation for you?
Address
CHPP Engineering title graphic featuring bold white text reading "CHPP Engineering" centred on a blue rounded rectangle background.
Pipework Drafting title graphic featuring bold white text reading "Pipework Drafting" centred on a blue rounded rectangle background.
3D LiDAR Scanning for Engineering Projects title graphic featuring bold white text on a blue rounded rectangle background.
3D CAD Modelling Australia service banner for Hamilton By Design

Designing Bucket Elevators vs Pan Conveyors in Industrial Material Handling

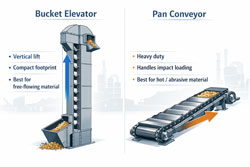
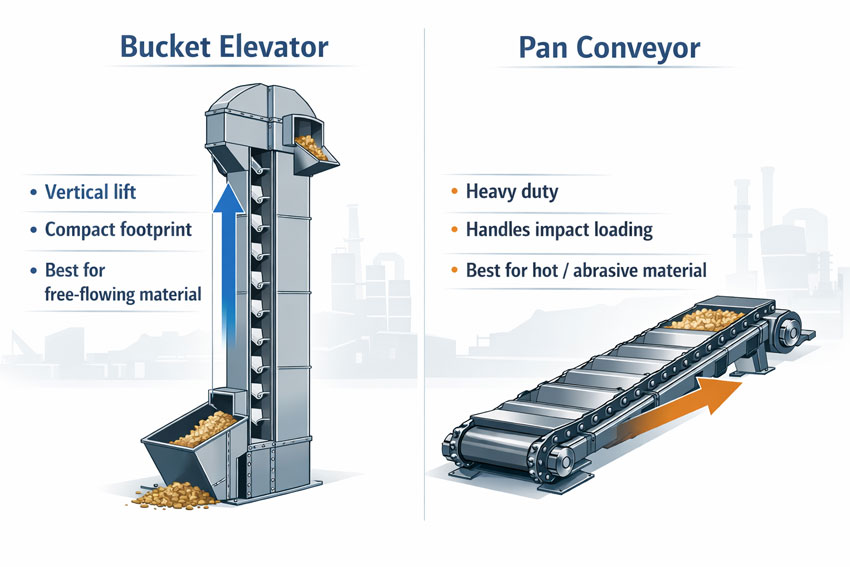
Engineering comparison diagram showing a bucket elevator lifting bulk material vertically and a pan conveyor transporting material horizontally.

Bucket Elevator vs Pan Conveyor Design | Industrial Material Handling Engineering

In bulk material handling industries such as mining, cement production, grain processing, and industrial manufacturing, selecting the right conveying system is critical to reliability, maintenance efficiency, and operating cost. Two commonly used systems are bucket elevators and pan conveyors. While both systems move bulk material efficiently, they are designed for very different operating conditions and material characteristics.

Understanding the difference between the two systems helps engineers select the correct solution for the application.


Bucket elevator vs pan conveyor industrial material handling comparison infographic.

What is a Bucket Elevator?

A bucket elevator is a vertical conveying system designed to lift bulk materials using a series of buckets attached to either a belt or chain. The buckets scoop material from the boot section and carry it upward to the discharge point.

Bucket elevators are widely used where material must be lifted vertically in a compact footprint.

Key Components

Buckets (steel, nylon, or HDPE)
Belt or chain drive
Boot section (material inlet)
Head section with drive and discharge
Casing or elevator trunking

Typical Applications

Grain handling
Fertiliser plants
Cement and lime processing
Mining concentrate handling
Sand, ash, or powder transport

Advantages

Efficient vertical lifting
Small plant footprint
High throughput capacity
Energy efficient for vertical transport

Limitations

Not ideal for very abrasive or large lump materials
Sensitive to overloading and blockages
Requires careful alignment and maintenance


What is a Pan Conveyor?

A pan conveyor, often called an apron conveyor, transports material horizontally or on shallow inclines using overlapping steel pans attached to heavy-duty chains.

The pans form a continuous moving surface that carries material along the conveyor frame.

Pan conveyors are commonly used in harsh industrial environments where materials are heavy, hot, or abrasive.

Key Components

Steel pans or plates
Heavy-duty conveyor chains
Sprockets and drive system
Conveyor frame
Impact loading zone

Typical Applications

Clinker transport in cement plants
Mining ore handling
Hot ash handling
Crusher discharge conveyors
Furnace feed systems

Advantages

Handles very heavy and abrasive materials
Suitable for impact loading
Reliable in harsh environments
Can operate at slow controlled speeds

Limitations

Larger footprint
Higher capital cost
More power consumption than bucket elevators


Key Differences Between Bucket Elevators and Pan Conveyors

Bucket Elevator
Vertical conveying system
Best for fine to medium bulk materials
Compact footprint
High energy efficiency for vertical transport
Requires controlled loading

Pan Conveyor
Horizontal or inclined conveying system
Handles heavy, abrasive or hot materials
Larger footprint
More robust construction
Handles high impact loading


When to Choose a Bucket Elevator

A bucket elevator is typically the preferred solution when:

Material must be lifted vertically
Plant space is limited
The material is free-flowing
Throughput is high but impact loading is low

Examples include grain silos, cement plants, fertiliser plants, and powder handling systems.

In these situations, bucket elevators provide a compact and energy-efficient solution.


When to Choose a Pan Conveyor

A pan conveyor is the better choice when:

Material is coarse, hot, or abrasive
There is high impact loading
The conveyor must operate continuously in harsh conditions
Reliability is more important than plant footprint

Examples include crusher discharge conveyors, furnace feed systems, clinker transport, and mining ore handling.

Pan conveyors are designed to survive the harshest bulk material handling environments.


Engineering Design Considerations

When designing either system, engineers must consider the following:

Bulk material characteristics
Lump size distribution
Abrasiveness
Moisture content
Throughput requirements
Loading conditions
Maintenance access
Structural support

Modern projects often integrate 3D laser scanning and point cloud modelling to ensure conveyors fit within existing plants and connect correctly to existing infrastructure. This approach reduces installation risk and helps engineers verify clearances, structural loads, and maintenance access before fabrication.

3D LiDAR scanning and 3D modelling service button โ€” laser scanner capturing a point cloud for engineering and CAD modelling
Mechanical engineering services

Hamilton By Design logo displayed on a blue tilted rectangle with a grey gradient background

Engineering Support for Conveyor Design

Hamilton By Design supports industrial projects with:

Mechanical conveyor design
3D laser scanning of existing plants
Conveyor chute and transfer design
Structural steel and support frames
Inspection and maintenance optimisation

Whether designing a bucket elevator for vertical material handling or a heavy-duty pan conveyor for mining operations, selecting the correct system is critical to long-term reliability and operational efficiency.


Name
Would you like us to arrange a phone consultation for you?
Address
3D CAD Modelling Australia service banner for Hamilton By Design
Australian Drafting logo featuring bold white text reading "Australian Drafting" centred on a blue rounded rectangle background.
Engineering Governance title graphic featuring bold white text reading "Engineering Governance" centred on a blue rounded rectangle background.
Mechanical, Structural & Pipework Drafting service banner by Hamilton By Design featuring white text on a blue background.
Mechanical engineering services
Blue rounded button with the text โ€œSolidWorks Designโ€ in white.
Finite Element Analysis (FEA) engineering simulation button
3D LiDAR Scanning Darwin for engineering surveys, laser scanning, reality capture and point cloud modelling services
3D LiDAR Scanning Australia engineering services for laser scanning, reality capture, scan-to-CAD, Scan-to-BIM and as-built documentation across Australia
3D LiDAR scanning services on the Central Coast providing engineering-grade laser scanning, point cloud capture, scan-to-CAD modelling and industrial reality capture for infrastructure and industrial projects.
3D LiDAR Scanning Perth for engineering surveys, laser scanning, reality capture and point cloud modelling services
3D LiDAR Scanning Sydney for engineering surveys, laser scanning, reality capture and point cloud modelling services
3D LiDAR Scanning Brisbane for engineering surveys, laser scanning, reality capture and point cloud modelling services
3D LiDAR Scanning Canberra for engineering surveys, laser scanning, reality capture and point cloud modelling services
3D LiDAR Scanning Newcastle for engineering surveys, laser scanning, reality capture and point cloud modelling services
3D LiDAR Scanning Adelaide for engineering surveys, laser scanning, reality capture and point cloud modelling services

AS 4324.1 Brownfield Bulk Handling Assets: Engineering Mobile Equipment for Todayโ€™s Mine Sites

AS 4324.1 Bulk Handling Equipment | Brownfield Stacker & Reclaimer Engineering

Mobile equipment for the continuous handling of bulk materialsโ€”such as stackers, reclaimers, and ship loadersโ€”forms the backbone of Australiaโ€™s mining and export infrastructure. Many of these assets operate continuously in demanding environments, often well beyond their original design life.

Australian Standard AS 4324.1 provides essential guidance for the design and safe operation of this class of equipment. However, on many Australian mine sites, the practical application of the standard is misunderstood or only partially implemented, particularly when dealing with legacy machines and brownfield upgrades.

For asset owners and engineering managers, the challenge is rarely about greenfield compliance. It is about managing risk, extending asset life, and implementing upgrades without unplanned downtime.


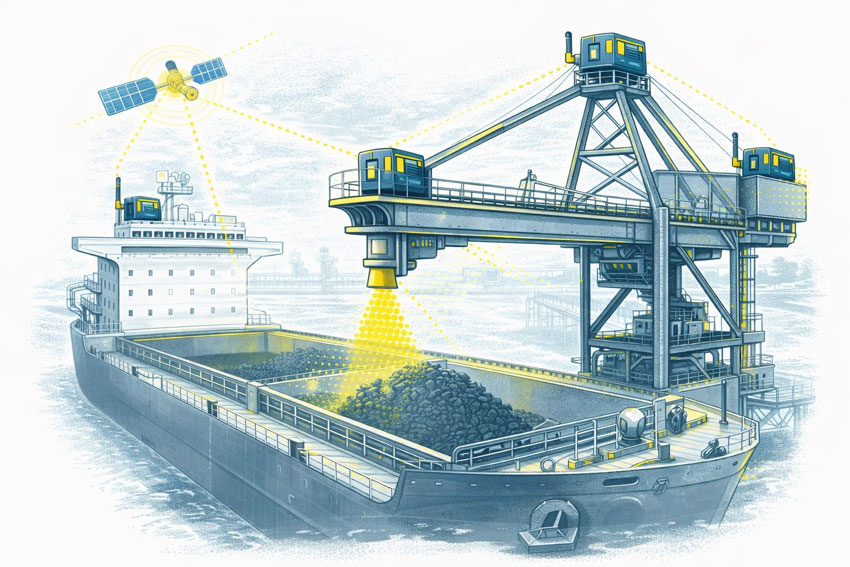
Ship loader and bulk cargo vessel with GPS monitoring units and sensor overlays illustrating controlled loading zones and engineering oversight under AS 4324.1

Understanding AS 4324.1 in a Brownfield Context

AS 4324.1 addresses mobile equipment used for continuous bulk handling, including:

  • Yard stackers and reclaimers
  • Bucket wheel reclaimers
  • Slewing and travelling machines
  • Ship loaders at export terminals

While the standard establishes a strong baseline for design and safety, many operating machines:

  • Pre-date the current revision of the standard
  • Have undergone multiple undocumented modifications
  • Operate under loading conditions that differ from original assumptions

In these situations, engineering judgement is required. Compliance becomes less about box-ticking and more about demonstrating that risks are understood, controlled, and managed over the asset lifecycle.


Common Challenges on Operating Mine Sites

Across coal handling plants, iron ore operations, and port facilities, several recurring issues emerge:

1. Incomplete or Outdated As-Built Information

Accurate geometry, slew limits, clearances, and structural interfaces are often unknown. This creates risk during upgrades and maintenance planning.

2. Fatigue and Structural Degradation

Large mobile machines experience cyclic loading across slewing, luffing, and travel motions. Fatigue cracking and unexpected failures require ongoing monitoring, not one-off assessments.

3. Access, Guarding, and Maintenance Compliance

Requirements evolve over time. Older machines may not meet current expectations for access systems, guarding, or safe maintenance practices.

4. Downtime Sensitivity

Stackers, reclaimers, and ship loaders are often production-critical assets. Upgrade windows are limited, and poor fit-up or rework can have significant commercial consequences.


Technology Supporting Modern Risk Management

While AS 4324.1 remains the foundation, modern technology allows asset owners to manage risk more effectivelyโ€”particularly on brownfield equipment.

GPS Positioning and Controlled Operating Zones

Where GPS positioning is enabled, defined operating zones can be established to:

  • Prevent interaction with stockpiles during rapid translation
  • Automatically reduce slew or travel speed in high-risk zones
  • Limit impact loads on critical components such as slew rings and fluffing gears

These systems are primarily productivity-driven, but they also reduce the likelihood of high-energy impacts that contribute to mechanical damage.


LiDAR Scanning as an Emerging Risk Layer

LiDAR scanning is not a replacement for traditional controls, and it is still evolving in this application. However, it can provide:

  • Accurate spatial awareness of surrounding structures
  • Verification of clearances and exclusion envelopes
  • A secondary risk-management layer supporting operator decision-making

When combined with engineering-led interpretation, LiDAR contributes to a layered risk approach rather than acting as a standalone safety system.


Condition Monitoring and Real Load Understanding

Accelerometers installed across a range of frequencies can deliver valuable insight into:

  • Actual operating loads
  • Dynamic response during slewing, reclaiming, and travel
  • Early indicators of fatigue-related issues

This data supports more informed maintenance decisions and provides evidence of how a machine is truly being usedโ€”often revealing load cases not considered in original designs.


Engineering-Led Compliance and Asset Life Extension

For brownfield assets, compliance with AS 4324.1 is best approached as a continuous engineering process, not a single milestone. This includes:

  • Accurate reality capture and digital models
  • Verification of clearances, interfaces, and structural geometry
  • Informed upgrade design that fits the first time
  • Risk-based decision-making supported by real operating data

This approach helps asset owners extend the life of critical machines while managing risk, performance, and availability.


How Hamilton By Design Supports Bulk Handling Assets

Hamilton By Design works with asset owners and engineering teams to support:

  • Brownfield upgrades of stackers, reclaimers, and ship loaders
  • Engineering-grade LiDAR scanning and as-built documentation
  • Fit-for-purpose mechanical design for modifications and life-extension
  • Independent engineering insight across OEM and site interfaces

Our focus is on engineering clarity, practical risk reduction, and minimising disruption to operations.


Talk to an Engineer About Your Asset

If you are planning a brownfield upgrade, life-extension, or risk review of mobile bulk-handling equipment, talk to an engineer at Hamilton By Design about how accurate data and practical engineering can support your next decision.

Hamilton By Design logo displayed on a blue tilted rectangle with a grey gradient background
3D LiDAR scanning and 3D modelling service button โ€” laser scanner capturing a point cloud for engineering and CAD modelling
Mechanical engineering services

Our clients:
Name
Would you like us to arrange a phone consultation for you?
Address
Finite Element Analysis (FEA) engineering simulation button
Mechanical engineering services

Mechanical Engineering for Australiaโ€™s Mining Sector

3D laser scanner capturing point cloud data of remote processing plant.

Mechanical Engineering for Australiaโ€™s Mining Sector

Blue Gear and Spanner icon

Hamilton By Design brings practical mechanical engineering expertise to Australiaโ€™s mining industry โ€” designed to help operators, maintenance teams and engineers improve reliability, meet compliance standards, and enhance on-site performance.

Mining operations demand robust mechanical systems that operate safely within tight production windows and regulatory frameworks. Our engineering approach is built on real-world understanding of mining workflows, heavy equipment mechanics and statutory requirements for above-ground and processing environments across Australia. Hamilton By Design Co.

What We Offer for Mining Clients

We deliver mechanical engineering services focused on improving plant uptime, operational safety and asset integrity, including:

  • Design & optimisation of mechanical components such as custom chutes, conveyors, wear liners and process equipment
  • Engineering support for maintenance and refurbishment, ensuring rebuilds and upgrades meet functional and compliance criteria
  • Mechanical risk evaluation and mitigation, with structured recommendations aligned to Australian mining safety standards
  • Asset inspection coordination and detailed reporting, enabling data-informed decisions for repairs or replacements
  • Documentation for fabrication and installation, including CAD models and engineering specifications tailored to site conditions

Our services are structured to support mining businesses at every stage โ€” from early project planning to on-ground solutions that reduce unplanned outages and improve asset performance. Hamilton By Design Co.

Expertise Rooted in Industry Experience

Hamilton By Designโ€™s mechanical engineering team combines practical site experience with advanced tooling such as 3D CAD modelling, laser scanning and engineering analysis. Whether your challenge involves enhancing mechanical reliability or integrating new equipment into an operating facility, our solutions are engineered for safety, precision and longevity. Hamilton By Design Co.

Why Partner With Us

Mining organisations choose Hamilton By Design because we:

  • Understand the specific mechanical demands of mining operations across Australia
  • Deliver compliant, build-ready engineering outcomes aligned with operational targets
  • Use advanced measurement and modelling technologies to reduce rework and site risks
  • Offer responsive engineering support tailored to your production timetable

From initial scoping through to detailed engineering documentation and implementation support, we help mining businesses solve mechanical challenges with effective, practical design solutions

Hamilton By Design logo displayed on a blue tilted rectangle with a grey gradient background
3D LiDAR scanning and 3D modelling service button โ€” laser scanner capturing a point cloud for engineering and CAD modelling
Mechanical engineering services

Our clients:
Name
Would you like us to arrange a phone consultation for you?
Address

3D Scanning Sydney banner promoting engineering-grade 3D laser scanning, LiDAR scanning, and reality capture services by Hamilton By Design.
Mechanical Engineering Sydney banner with white text on a blue background representing Hamilton By Design's mechanical engineering services in Sydney.
Mechanical Drafting and 3D Modelling Sydney banner highlighting Hamilton By Design's CAD drafting, 3D modelling, and engineering design services in Sydney.

Mechanical Engineering | Structural Engineering